(650) 522-4653

2026 Top Bourbon Filtration Equipment for Global Buyers?

Choosing the right equipment for bourbon filtration requires more than comparing prices and polished product brochures. Global buyers need reliable performance, documented materials, and support that continues after installation. This introduction examines leading filtration systems expected to attract attention in 2026, including cartridge filters, depth filters, membrane systems, and complete skid-mounted units.

Real production conditions matter. A stainless steel housing may look excellent, yet its seals can fail under repeated cleaning cycles. A precise micron rating may also change when flow rates, temperature, or spirit viscosity increase. Buyers should review pressure limits, food-contact certifications, clean-in-place compatibility, replacement-part availability, and supplier testing records. Small details often decide whether a system performs smoothly beside a bottling line or causes repeated production delays.

No equipment is perfect. Some suppliers provide strong engineering but limited regional service. Others offer low prices, while documentation remains incomplete. That weakness deserves attention. A dependable evaluation should include factory experience, installation references, laboratory data, and clear warranty terms. It should also respect local safety rules, environmental requirements, and responsible production standards in every destination market.

This guide presents practical selection criteria for bourbon filtration equipment in 2026. It focuses on measurable performance, operational reliability, maintenance demands, and total ownership cost. Buyers can use these points to compare suppliers with greater confidence, while recognizing that site conditions may require independent technical verification. Good decisions begin with evidence, not slogans.
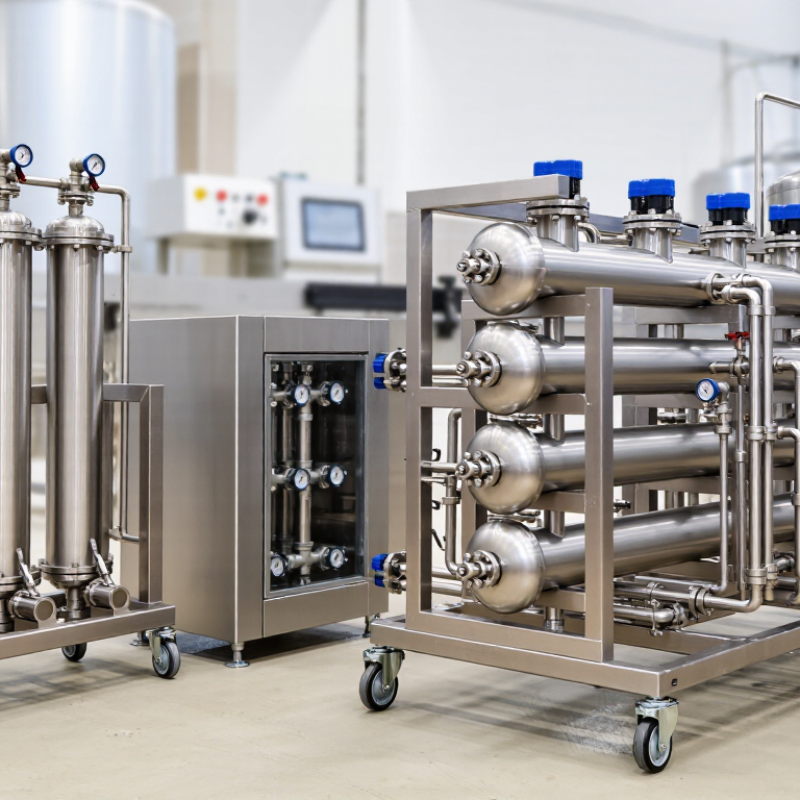
2026 Top Bourbon Filtration Equipment for Global Buyers?

Bourbon Filtration Equipment: Purpose, Types, and Core Principles

Bourbon filtration equipment helps producers control clarity, sediment, and texture before bottling. In a working distillery, operators may see haze after cooling or fine char particles in a transfer line. Filtration removes unwanted solids without stripping every aroma. It does not repair poor maturation or unstable blending. That distinction matters when buyers compare equipment for 2026 production plans. Experience on the floor shows that a clean filter housing, steady flow, and measured pressure often matter as much as capacity.

Common systems include cartridge filters, depth filters, plate-and-frame units, and membrane systems. Cartridge filters suit final polishing and compact lines. Depth filters handle heavier solids, but they need careful pre-rinsing. Plate systems offer flexible surface area for medium or large batches. Membranes provide finer separation, yet they can foul quickly when the spirit carries oils or residual solids. Selection should follow batch size, target proof, viscosity, cleaning method, and local service access. A large system is not automatically better.

Filtration works through size exclusion, adsorption, and depth capture. Pressure must remain within the housing specification. Excessive pressure can compact the media and slow the process. Operators should record inlet pressure, outlet pressure, temperature, flow rate, and alcohol strength for each run. Food-contact materials, traceable seals, and validated cleaning procedures support dependable operation. Some decisions remain imperfect. A filter may improve brightness while softening a desired mouthfeel. Small pilot trials and sensory checks are wiser than trusting a specification sheet alone.
2026 Top Bourbon Filtration Equipment for Global Buyers

Typical filtration fineness by equipment type, expressed as the approximate particle-size rating in micrometres (µm). Lower values indicate finer filtration.

Coarse strainers remove visible solids before polishing. Depth and cartridge filters are commonly used for particulate removal, while membrane systems provide the finest separation when process design, pressure, and product compatibility allow. Actual ratings vary by filter media, bourbon temperature, viscosity, and required flow rate.

Key Specifications for Comparing Bourbon Filtration Systems

Choosing bourbon filtration equipment requires more than comparing advertised flow rates. Global buyers should examine filtration media, micron rating, throughput, pressure limits, and product-contact materials. A system rated for 5–10 microns may remove visible particles, while finer filtration can affect clarity and yield. Stainless steel construction, food-grade seals, and documented surface finishes support safer, repeatable production.

Temperature control also matters. Bourbon can change viscosity during processing, influencing pressure and filtration speed. Look for operating ranges, pump compatibility, pressure gauges, and automatic shutoff features. Cleaning requirements deserve equal attention. Systems with practical clean-in-place connections can reduce downtime, but complicated piping may create hidden residue points. I have seen impressive equipment underperform because its actual flow rate was measured with water, not bourbon. That comparison can mislead.

Tips: Ask for test data using a similar liquid, not only laboratory water. Confirm electrical standards, spare-part access, installation space, and operator training before purchase. Review certificates for materials and pressure safety. A compact unit may suit a small facility, while a modular design offers easier expansion. However, bigger is not always better. Oversized equipment can increase product hold-up and cleaning time. Buyers should record target volume, desired clarity, acceptable loss, and cleaning frequency before comparing quotations. Specifications look precise, yet real-world results still need verification.

Top Bourbon Filtration Equipment Categories for Global Buyers in 2026

Global buyers in 2026 will need bourbon filtration equipment that matches production volume, spirit character, and site conditions.

The main category is depth filtration, using cellulose or other food-contact media to remove visible particles before filling. Plate-and-frame systems suit flexible batch production, while cartridge housings support faster changeovers and smaller footprints.

Membrane filtration offers finer polishing when clarity targets are strict. It can reduce haze without heavily changing aroma, but pressure control and cleaning procedures require careful planning.

Activated carbon systems may also be used in selected processes, although excessive contact can soften valuable flavor notes. Sanitary pumps, stainless-steel piping, and hygienic valves should be specified with the filtration unit.

Documentation matters too, including material certificates, flow data, cleaning guidance, and spare-part availability in the destination market.

Tips:

Ask suppliers for pilot-test results using your actual bourbon sample. Check throughput at realistic viscosity and temperature, not only ideal laboratory conditions. Confirm local power requirements, connection standards, and operator training.

A simple system is often easier to maintain. However, I would not assume the finest filter always delivers the best product. Taste trials, pressure logs, and repeated batch comparisons remain essential, especially when equipment will serve different warehouses or climates.

Installation, Operation, and Maintenance Requirements

Choosing top bourbon filtration equipment in 2026 requires more than comparing flow rates. Installation quality often determines final performance. The system should use food-grade contact materials and match the distillery’s batch volume. Place it on a level, washable surface with enough space for filter changes. Keep hoses short, supported, and clearly labeled. A rushed installation may look successful for one shift. That is not enough.

During operation, trained staff should check inlet pressure, outlet pressure, temperature, and flow consistency. Record these readings for every batch. Sudden pressure changes may indicate blocked media, trapped air, or an incorrect valve position. Operators should inspect sight glasses before starting the pump. Start slowly, then increase flow within the equipment’s documented limits. I have seen teams focus on speed and miss small leaks near fittings. That mistake becomes expensive.

Maintenance should include cleaning, approved sanitation procedures, gasket inspection, and scheduled filter replacement. Follow the manufacturer’s technical instructions and local workplace requirements. Never treat a visual inspection as a complete safety check. Test instruments should be calibrated at defined intervals. Records should include dates, readings, cleaning agents, replacement parts, and staff initials. Some facilities still keep incomplete logs. That weakness needs attention.

Tips: Keep spare seals, clamps, and compatible filter elements nearby. Mark normal pressure ranges beside the control panel. Train operators with a real cleaning demonstration, not only a manual. Review maintenance records monthly and investigate repeated pressure problems. Safety glasses and suitable protective gloves should be available during servicing.

2026 Top Bourbon Filtration Equipment for Global Buyers? - Installation, Operation, and Maintenance Requirements

A practical comparison of common filtration equipment used for bourbon and other distilled spirits, including typical process ranges and purchasing requirements.

Equipment Category Primary Bourbon Application Typical Filtration Rating or Separation Range Typical Capacity Installation Requirements Operating Requirements Maintenance Requirements Key Global-Buyer Selection Criteria
Depth Filter System Removal of coarse particles, carbon fines, barrel debris, and visible sediment before final polishing. Approximately 1–20 micrometres, depending on the filter media and process configuration. Commonly 500–5,000 L/h for small and medium production lines. Install on a level, washable floor with sanitary product piping, drain access, and sufficient clearance for media or cartridge replacement. Control flow to prevent channeling and excessive pressure rise. Monitor inlet and outlet pressure during each production run. Replace filter media when the differential pressure reaches the supplier’s limit or when flow declines. Sanitize product-contact surfaces after use. Food-contact materials, low product hold-up, compatible gaskets, local electrical compliance, and availability of replacement media.
Bag Filter Housing Pre-filtration of suspended solids and protection of downstream cartridge or membrane filters. Typically 1–100 micrometres, based on the selected bag and housing configuration. Approximately 1,000–20,000 L/h, depending on housing size, viscosity, and pressure loss. Provide vertical access for bag removal, a sanitary drain, pressure gauges, and a bypass or isolation arrangement where required. Operate within the housing pressure rating. Avoid exceeding the recommended flow rate, especially with high-solids bourbon. Inspect the housing, clamp, lid seal, and basket regularly. Replace bags rather than attempting to reuse disposable media unless specifically designed for reuse. 316L stainless steel product-contact parts, easy-open cover, secure bag retention, pressure rating, and standardized bag dimensions.
Cartridge Filter Skid Final polishing to improve visual clarity and remove fine suspended particles before bottling. Common nominal or absolute ratings from approximately 0.45–10 micrometres. Approximately 500–10,000 L/h, depending on cartridge count, viscosity, and filter area. Install with sanitary tubing, sample ports before and after filtration, pressure gauges, drain points, and adequate space for cartridge removal. Use a staged arrangement, normally coarse filtration followed by finer filtration. Keep the product temperature stable to avoid viscosity-related flow changes. Change cartridges at the specified differential pressure or validated batch limit. Inspect O-rings and sanitize the housing between compatible product campaigns. Cartridge availability in the destination market, validated retention rating, low extractables, sanitary connections, and documented integrity information.
Plate-and-Frame Filter Press Batch clarification of bourbon containing relatively high levels of suspended solids. Commonly about 1–20 micrometres, depending on filter sheets and cellulose depth media. Approximately 500–10,000 L per batch; actual output depends on solids loading and filter area. Requires a stable support frame, drip tray, product pump, filtrate collection, drainage, and safe access for opening the plate pack. Precoat or load filter sheets correctly. Increase pressure gradually and remain within the plate, gasket, and sheet specifications. Wash and sanitize plates, inspect gaskets for swelling or damage, and replace filter sheets after each batch unless the process is validated for reuse. Food-grade plate materials, reliable clamping system, sheet availability, operator safety, and compatibility with the selected cleaning chemicals.
Cross-Flow Microfiltration System Continuous or semi-continuous clarification with reduced filter-media consumption and controlled solids buildup. Often approximately 0.1–1.0 micrometres for microfiltration membranes. Approximately 500–10,000 L/h, depending on membrane area, temperature, solids concentration, and viscosity. Needs a recirculation loop, feed tank, sanitary pump, membrane housing, permeate and concentrate lines, instrumentation, and a suitable clean-in-place connection. Maintain validated cross-flow velocity, transmembrane pressure, temperature, and feed flow. Avoid operating with an empty membrane or uncontrolled pressure spikes. Perform rinse, alkaline cleaning, and periodic acidic cleaning when compatible with the membrane. Track permeability and replace membranes when performance cannot be restored. Membrane material compatibility with ethanol, cleaning agents, and flavor compounds; automation level; energy use; and technical support in the operating region.
Activated-Carbon Treatment Unit Reduction of selected color, odor, and flavor-active compounds when a controlled treatment step is required. Adsorption-based separation; performance depends on carbon type, contact time, particle size, and bourbon composition. Approximately 100–5,000 L/h for packed-bed or batch systems. Provide a protected vessel, dust control, explosion-risk assessment where applicable, sanitary piping, drainage, and a safe method for carbon loading and removal. Control contact time and flow distribution. Validate treatment carefully because excessive adsorption can remove desirable aroma and flavor compounds. Backwash or replace carbon according to validated capacity. Inspect for channeling, fines carryover, microbial growth, and pressure increase. Food-grade carbon documentation, combustible-dust controls, batch traceability, disposal arrangements, and a validated sensory and analytical protocol.
Chill-Filtration System Reduction of haze-forming components that may precipitate when bourbon is stored or served at lower temperatures. Uses controlled cooling followed by depth or cartridge filtration; the final rating commonly falls within approximately 1–10 micrometres. Approximately 500–10,000 L/h, depending on cooling duty, viscosity, and filter area. Requires a hygienic heat exchanger or jacketed tank, temperature control, insulation where needed, condensate management, and a downstream filter stage. Cool the spirit to a validated target temperature, allow adequate contact time, and maintain stable flow to prevent premature filter blockage. Clean the cooling circuit and product lines, verify temperature sensors, inspect seals, and replace blocked filter media according to differential pressure. Cooling capacity, energy efficiency, temperature uniformity, compatibility with ethanol service, hygienic design, and local refrigeration safety requirements.
Bottling-Line Final Filter Final particulate control immediately before filling to protect product appearance and filling equipment. Commonly 0.45–2.0 micrometres, selected according to product risk and validated flow requirements. Approximately 500–5,000 L/h for small and medium bottling operations. Install as close as practical to the filler using short sanitary lines, a hygienic housing, sample points, and a drainable configuration. Use a controlled, steady flow and avoid unnecessary recirculation that may increase oxygen pickup. Confirm filter integrity where applicable. Replace cartridges at the validated batch limit, sanitize the housing, inspect seals, and document filter lot, installation, and removal information. Low extractables, validated retention, oxygen-management compatibility, tamper-resistant installation, batch documentation, and rapid cartridge supply.
Procurement note: Actual performance depends on bourbon proof, temperature, solids loading, viscosity, dissolved oxygen targets, cleaning chemistry, and the validated process design. Buyers should request food-contact declarations, pressure and temperature ratings, material certificates, operating manuals, spare-parts lists, and commissioning support before purchase.

Global Purchasing Factors: Compliance, Costs, and Supplier Evaluation

Global bourbon filtration purchasing now depends on compliance, total cost, and supplier evidence. The 2024 Distilled Spirits Council industry report recorded 305.1 million nine-liter spirits cases in the United States during 2023. This scale increases pressure on filtration performance, cleaning speed, and production consistency. Buyers should request food-contact declarations, material certificates, pressure ratings, and documented hygienic design. Equipment touching bourbon must suit local requirements, including applicable FDA or European food-contact rules. Certification alone is not enough.

Cost comparisons should include membranes, filter media, labor, water, energy, spare parts, and disposal. A low quote can still become expensive. Ask suppliers for five-year operating estimates, not only purchase prices. Require pilot-test results using similar alcohol strength, color, and particulate loads. Performance claims without test conditions deserve caution. Global suppliers should explain lead times, installation support, remote diagnostics, and technician availability. ISO 9001 certification can support process confidence, but it cannot replace factory audits or reference checks.

Tips: Build a weighted supplier scorecard. Give compliance 30%, lifecycle cost 25%, filtration performance 25%, and service 20%. Check at least three customer references. Visit one operating site if possible. Review change-control procedures carefully. I would not assume the cheapest validated system is automatically the best choice; production interruptions are difficult to model, and every plant has different water quality, labor skills, and cleaning practices.

Contact Us

Phone: (650) - 522-4653 (GOLF)

Fax: (650) 522-7511

Tee Time Reservations: (650) 522-4653 (GOLF)

Location

1700 Coyote Point Drive

San Mateo, CA 94401